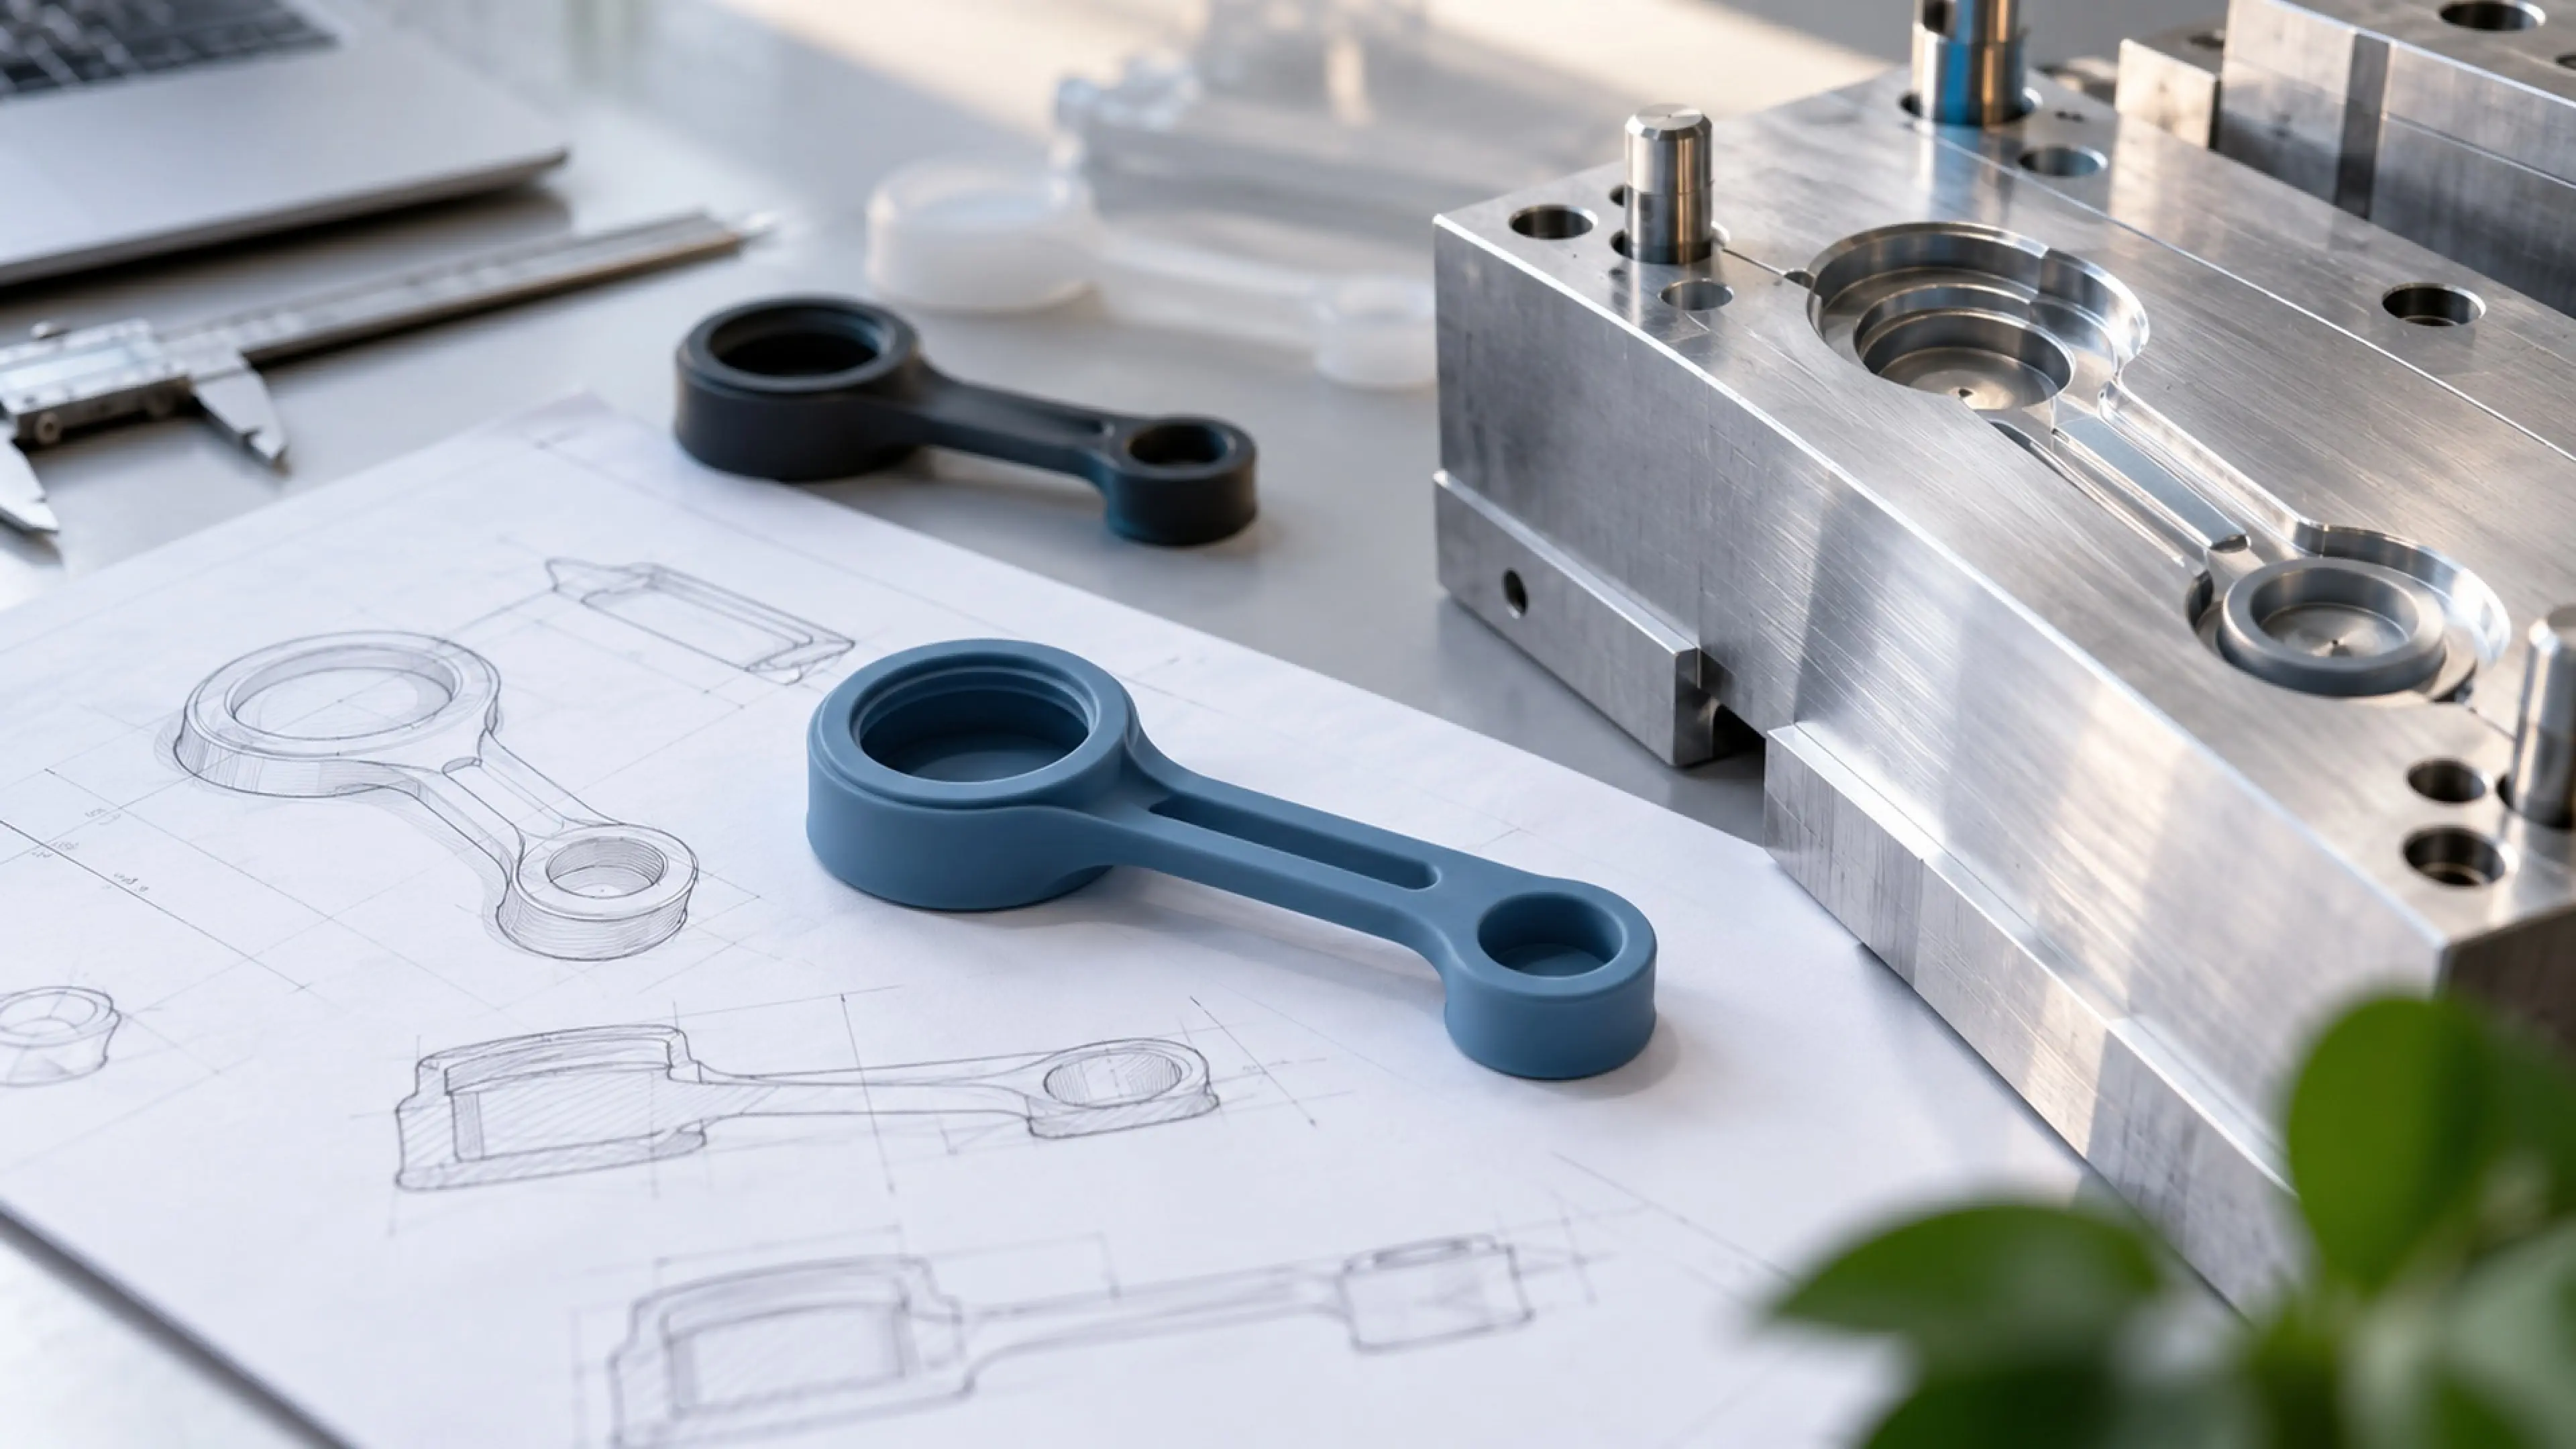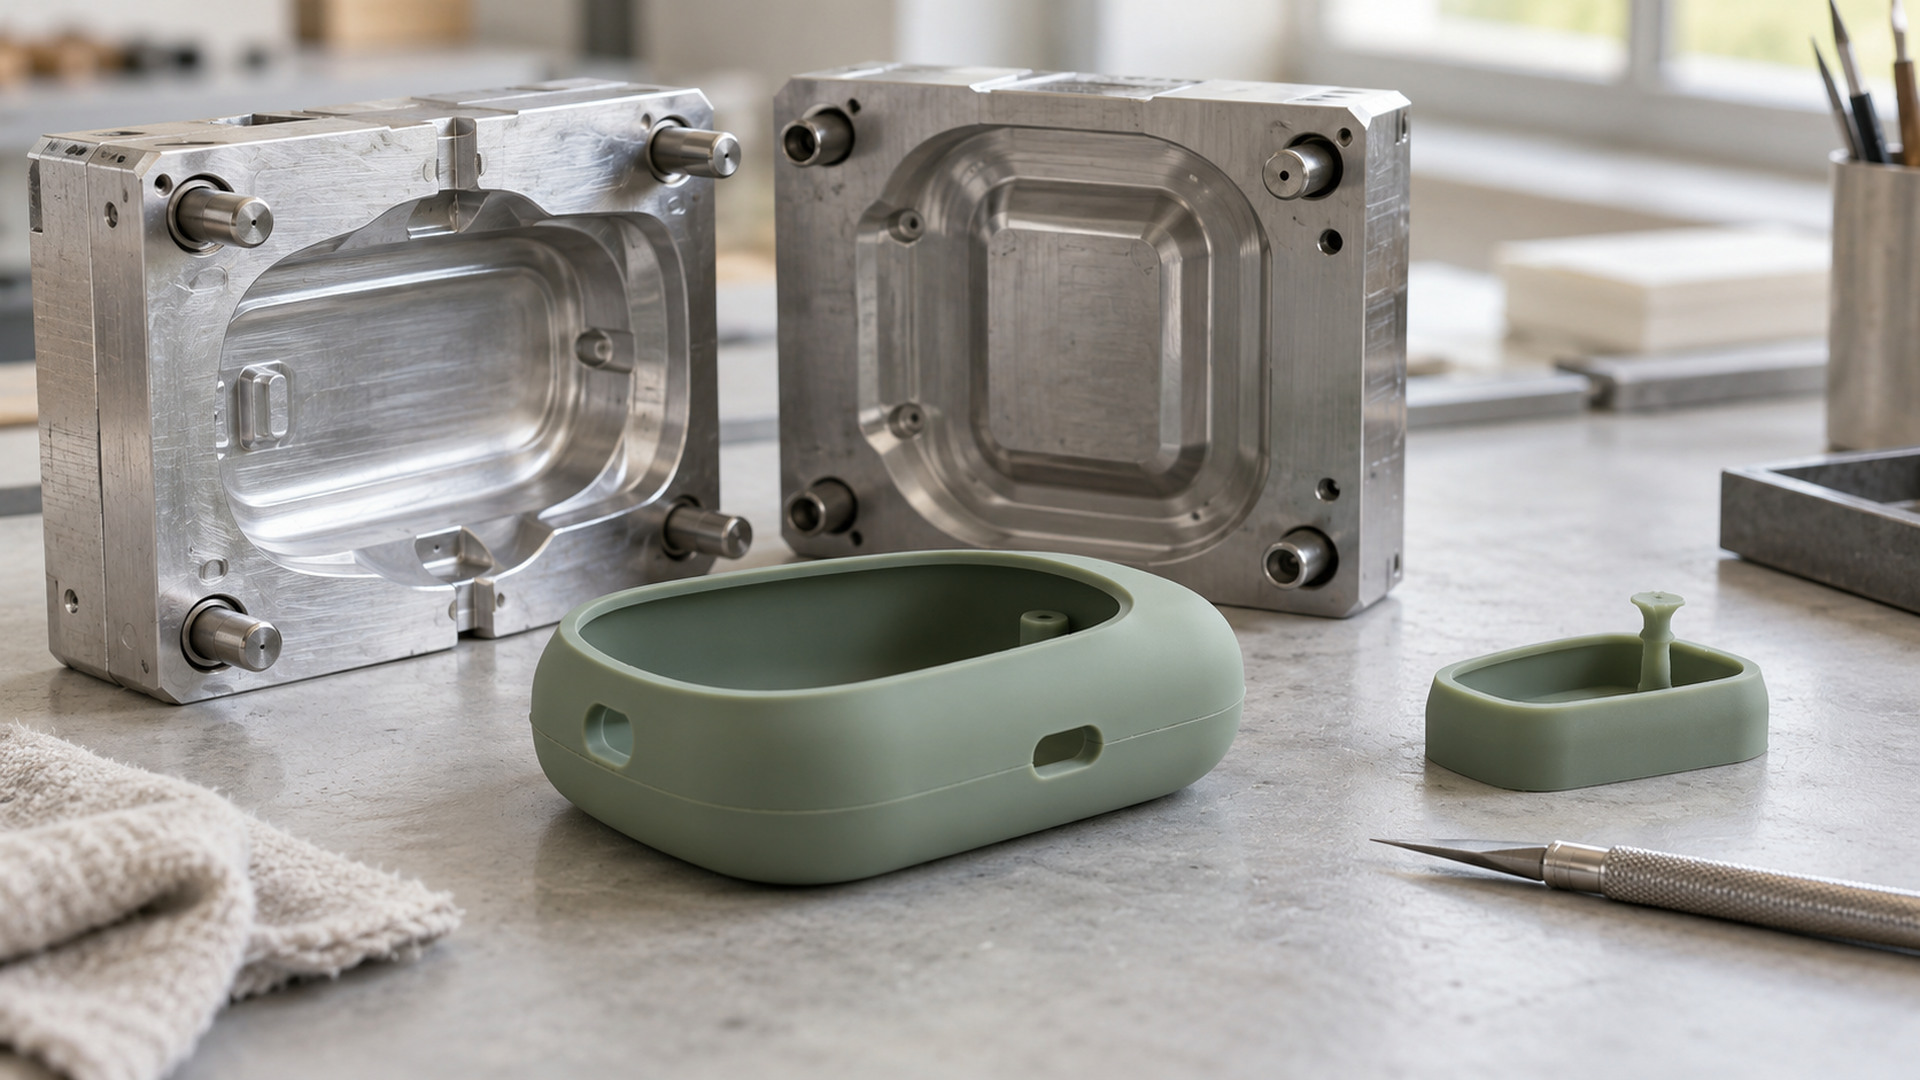
Where should parting lines and gates go to protect appearance and sealing?
Every molded silicone part carries the signature of its mold: a parting line where the two halves meet, and a gate mark where the material entered. Neither is avoidable — the question is where the factory puts them. Put them on a visible face and you get a visible seam; put them on a sealing land and you get a leak. Both decisions are made in the mold, before steel is cut.
The single most useful thing you can do is freeze which surfaces are cosmetic and which are functional before tooling. Once the parting line is machined into the steel, moving it means re-cutting.
The parting line is where the mold halves meet
The parting line is the natural seam between the cavity side and core side of the mold, and it is also where the thinnest flash tends to form. Two rules guide its placement:
- Keep it off cosmetic surfaces. A perfectly flash-free line still reads as a faint seam in the light. On a premium visible face, that seam is a defect; on a hidden edge or underside, it is invisible.
- Never run it across a sealing land. A parting line on the sealing surface creates a natural flash path and a micro-step that breaks the contact line the seal depends on. Design the seal so the land sits entirely on one mold half.
The parting line also sets the demolding direction. Choose it so the part releases cleanly and so undercuts the flexible silicone can manage are not turned into side-action problems.
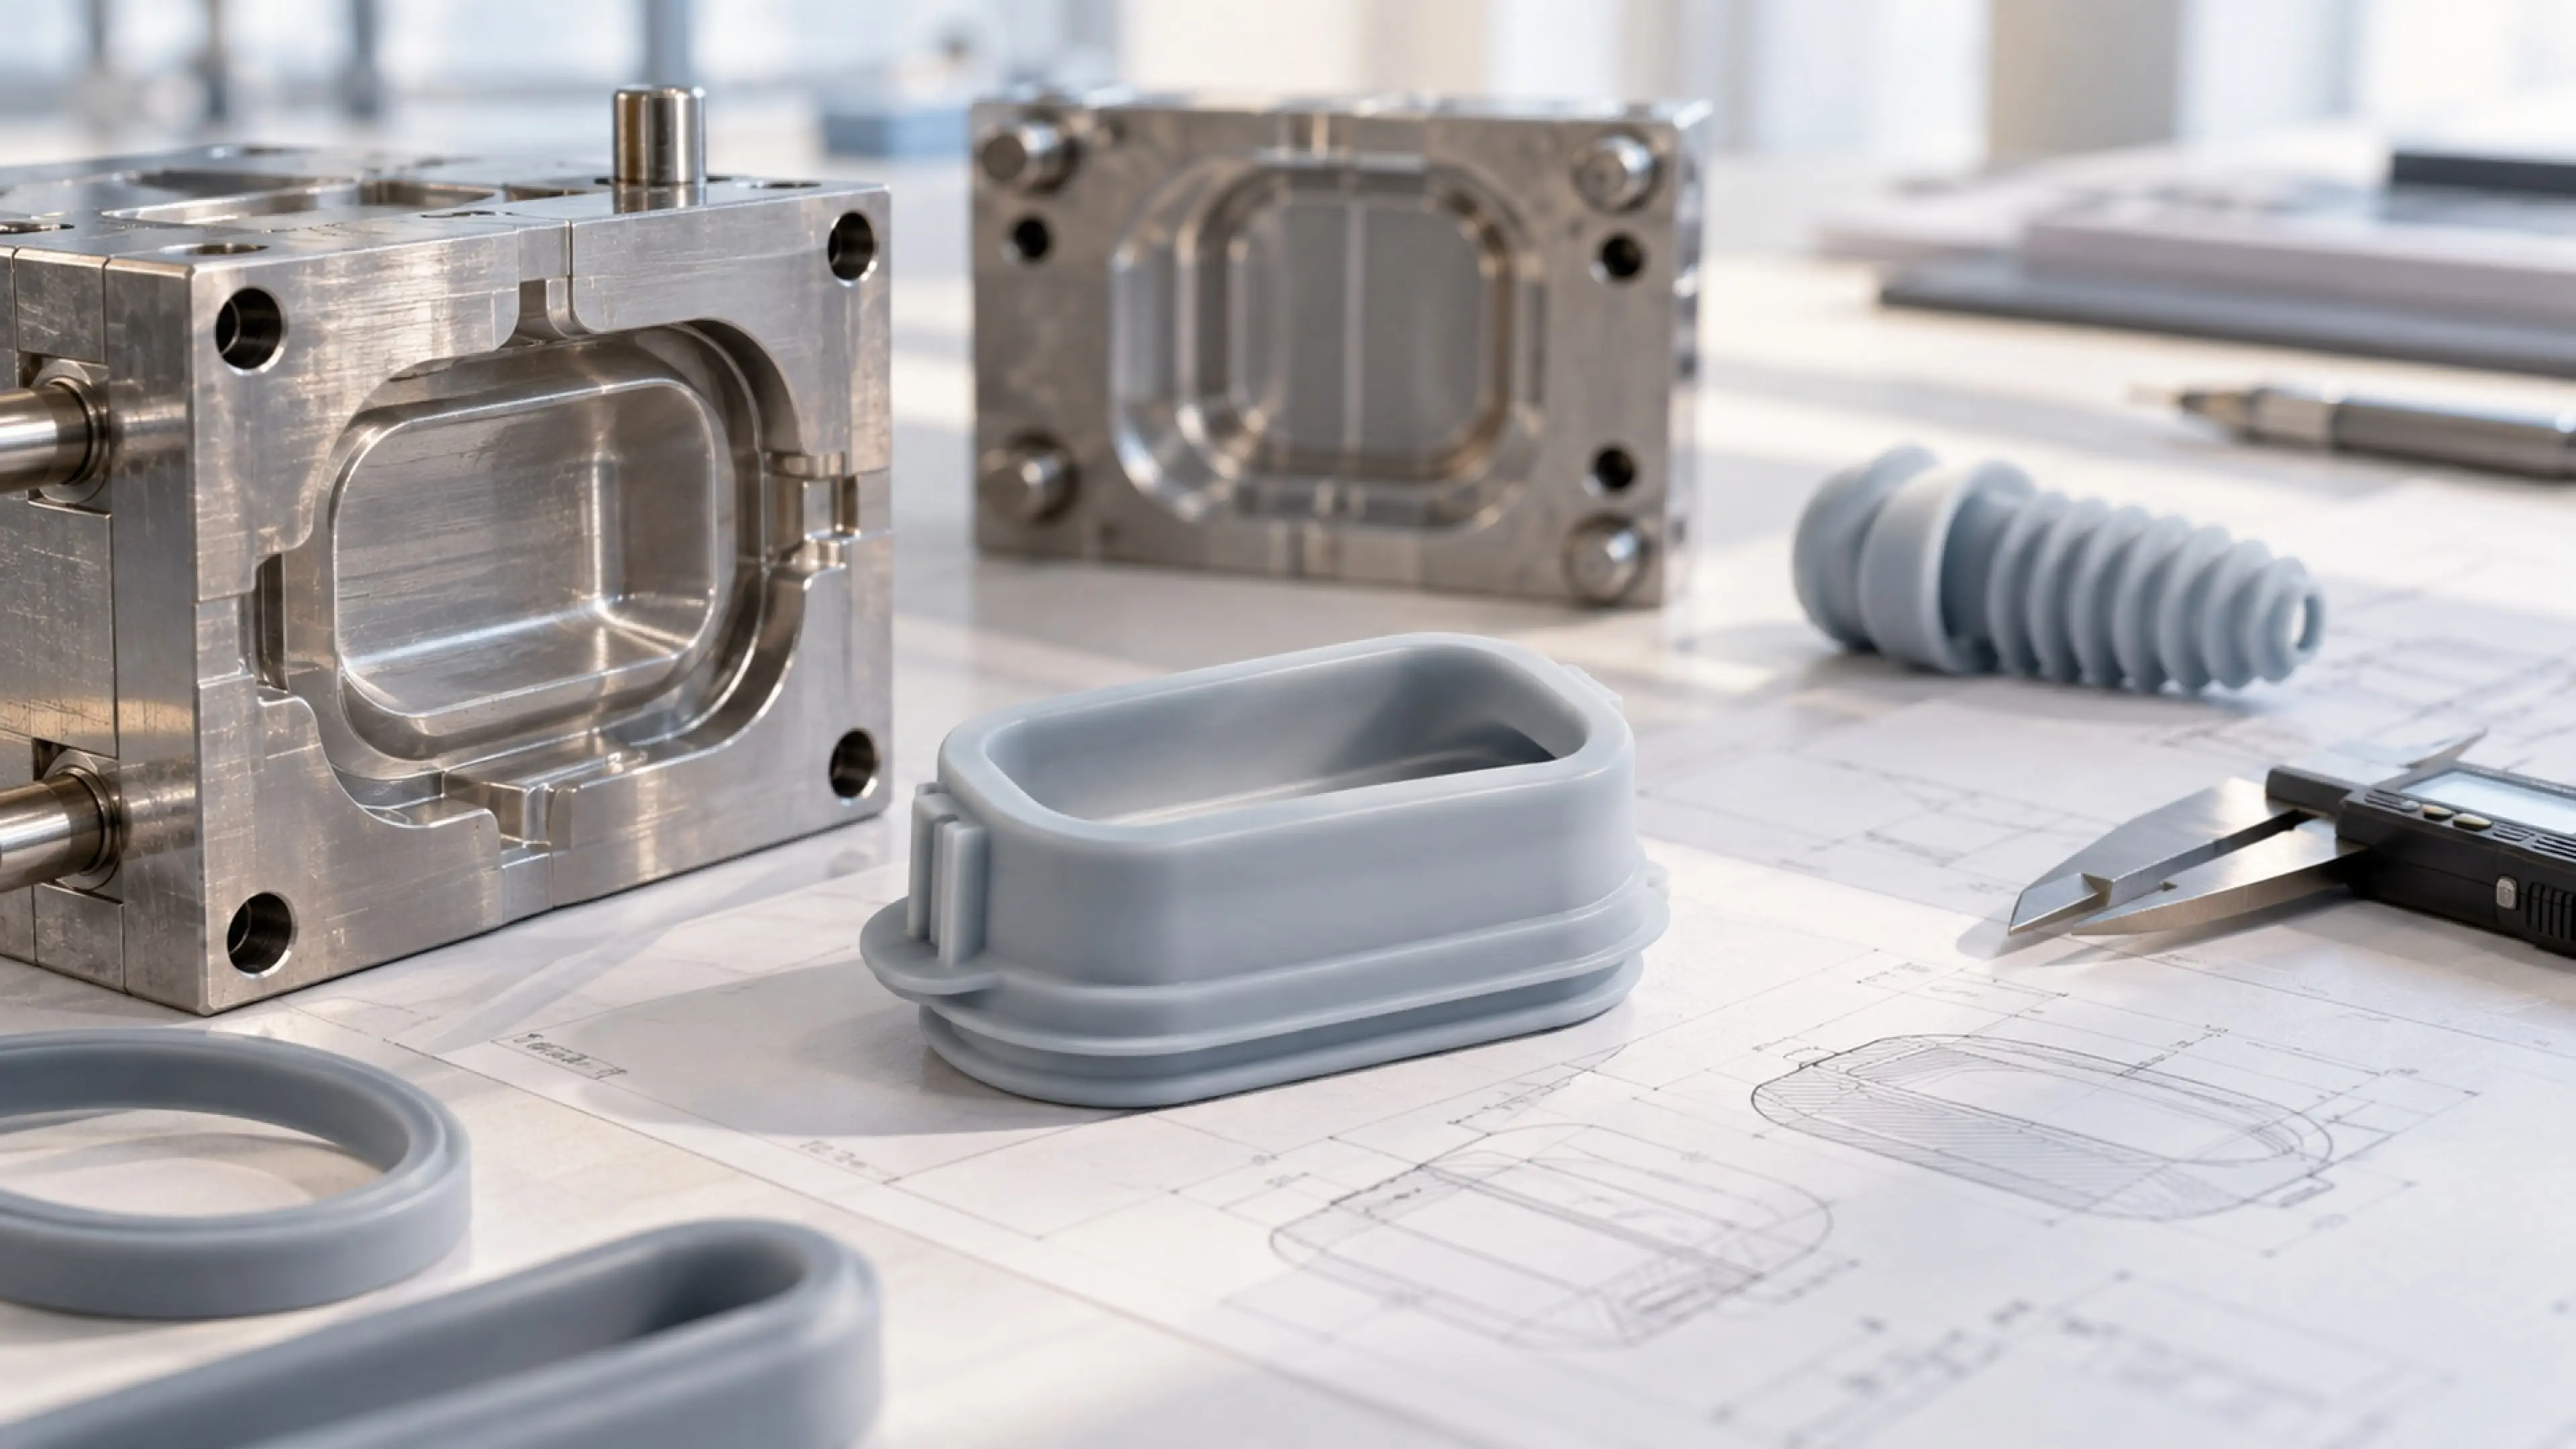
The gate leaves a vestige, too
In injection LSR, the gate is where the liquid enters the cavity. It leaves a small vestige that is trimmed, but the trim point is still visible on close inspection. As with the parting line:
- Place the gate on a non-cosmetic face where the vestige will not be seen.
- Keep it away from the sealing land and any precision mating surface.
- Let the mold designer size the gate and runner for balanced filling across cavities, since a poorly placed gate causes short shots or weld lines on the part.
On visible, brand-facing parts, ask the DFM review to show you exactly where both the parting line and gate will land, and sign off on that location.
Flash and venting follow the parting line
Where the mold halves meet is also where air has to escape. Venting strategy and flash control are designed around the parting line, which is why flash-prone cosmetic surfaces and tight sealing lands are poor places for it. Good tooling controls flash to near-invisible levels on LSR, but that control is designed in, not trimmed away after.
On cosmetic character or brand-facing parts, this choice is worth an explicit sign-off. A parting line that lands across a molded face or a logo is a defect no amount of hand-deflashing fully hides, and moving it later means re-machining the cavity. Mark the visible faces on the drawing early, and ask the mold designer to route the seam and gate to the hidden edge before approving the tool layout.
For a gasket, remember the seal is a component inside a larger device. Review tolerance stack-up, compression, and housing stiffness together, and validate the assembled device — a clean parting line in the right place only helps if the housing actually compresses the land.
Freeze the faces before steel
Before the mold is cut, review CAD and 2D drawings together and mark:
- Which faces are cosmetic, and where the parting line and gate will sit relative to them.
- Which faces are sealing or precision interfaces, off-limits to any seam.
- Critical dimensions that must hold on one mold half.
This is the DFM conversation that prevents a part that looks perfect in render but ships with a seam across the logo.
Turn vague language into an acceptance standard
"Clean look" or "no visible seam" is not inspectable. Convert intent into a written standard:
- A controlled reference — approved sample showing where the seam and gate vestige live.
- Critical characteristics — the sealing land, the cosmetic zone, and the appearance tolerance.
- A test condition — how flash is checked and how the seal is leak-tested.
- An acceptance rule — how much flash or vestige is acceptable where.
- A revision record — the parting-line and gate layout the approved sample came from.
Prototype parts, often hand-made, do not reveal where the production parting line will fall; only the tooled T1 sample does.
Questions to ask the supplier
- Where exactly will the parting line fall, and on which faces?
- Where will the gate vestige be, and can it land off the visible surface?
- Is the sealing land entirely on one mold half, away from the parting line?
- How do you control flash on the cosmetic surfaces?
- Can you show the parting-line and gate layout before steel is cut?
- How will flash and seal integrity be checked on each run?
Credible answers point to specific faces on your drawing. "It will be trimmed away" is not a placement decision.
Conclusion
Parting lines and gates are unavoidable, but their location is a choice made during tooling design. Keep both off cosmetic visible faces and — critically — off the sealing land, where a seam becomes a leak path. Freeze which faces are appearance and which are function before the mold is cut, and sign off on the seam and gate location on the DFM review. Moving them after steel is the expensive lesson.